

[WOKING PRINCIPLE AND FEATURES OF BAKING SODA MATERIAL CONVEYING LINES]
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material conveying lines for various industrial applications. This article provides an in-depth exploration of the working principle and key features of baking soda material conveying lines, highlighting the technological advancements and operational efficiency they offer.

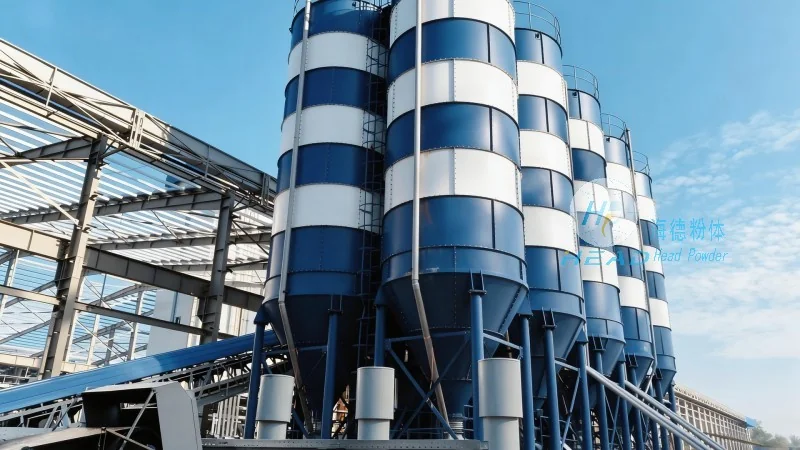
The core working principle of a baking soda material conveying line revolves around the integration of several mechanical and control components to ensure the safe and efficient transport of sodium bicarbonate (baking soda) from storage to processing or packaging areas. The system typically begins with a storage silo or hopper where the raw material is stored under controlled conditions to maintain its quality and prevent caking or moisture absorption.
From the storage hopper, the material is fed into a conveyor system, which may include screw conveyors, belt conveyors, or pneumatic conveying lines depending on the specific requirements of the application. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle bulk materials without the need for external power beyond the motor driving the screw. The screw, rotating within a U-shaped trough, moves the material forward by friction, ensuring a continuous and controlled flow. This method is particularly effective for transporting dry, free-flowing powders like baking soda, as it minimizes material degradation and maintains consistent product quality.

Belt conveyors, on the other hand, are often employed for longer horizontal distances or when a higher material capacity is required. The system consists of a continuous loop of belt supported by rollers, with the material placed on the belt and carried to the destination. This type of conveyor is suitable for both dry and slightly wet materials, providing a stable and reliable transport solution. For applications where vertical or steep incline transport is necessary, vertical screw conveyors or bucket elevators are utilized. These systems use a rotating screw or buckets to lift the material vertically, ensuring efficient movement even over significant height differences.
Pneumatic conveying systems represent another advanced method for transporting baking soda, especially in scenarios where dust control and flexibility are critical. This technology uses compressed air to create a flow that propels the material through a pipeline. The system typically includes a hopper, a rotary airlock valve to control material discharge, and a receiver at the destination. Pneumatic conveying offers advantages such as dust-free operation, reduced material degradation, and the ability to transport materials over long distances with minimal maintenance. However, it requires careful design to ensure proper air-to-material ratios and to prevent pressure drops that could affect performance.

Control systems play a vital role in the operation of baking soda material conveying lines, ensuring that the process is automated, efficient, and safe. Modern systems often incorporate PLC (Programmable Logic Controller) technology, which allows for precise control over the speed of conveyors, the flow rate of material, and the timing of various operational steps. Sensors are strategically placed throughout the system to monitor parameters such as material level, temperature, and pressure, providing real-time data to the control system. This enables proactive maintenance and immediate response to any deviations from normal operating conditions. Additionally, safety features such as emergency stop buttons, interlocks, and overload protection are integrated to prevent accidents and ensure compliance with industrial safety standards.
Key features of baking soda material conveying lines include high efficiency, low maintenance costs, and adaptability to various production environments. The systems are designed to handle large volumes of material with minimal energy consumption, making them cost-effective for industrial operations. The use of durable materials, such as stainless steel or corrosion-resistant alloys, ensures long service life and resistance to the chemical properties of baking soda, which can be slightly alkaline and may cause corrosion in some materials. The modular design of these conveying lines allows for easy installation, expansion, or modification to accommodate changes in production capacity or product specifications. This flexibility is particularly valuable for manufacturers that may need to adjust their operations based on market demand or new product lines.
Another important feature is the ability to maintain product purity and quality throughout the conveying process. Baking soda is a food-grade material, and any contamination or degradation can significantly impact its quality and usability. The conveying systems are designed with sealed components and minimal contact points to prevent cross-contamination from other materials or environmental factors. Additionally, the use of clean-in-place (CIP) systems allows for easy cleaning and sanitation, ensuring that the equipment remains hygienic and compliant with food safety regulations. This is particularly critical for industries where product quality and safety are paramount, such as food processing and pharmaceutical manufacturing.
The operational efficiency of baking soda material conveying lines is enhanced by the integration of automation and monitoring technologies. Real-time data collection and analysis enable manufacturers to optimize the system's performance, reduce downtime, and improve overall productivity. By monitoring key parameters such as conveyor speed, material flow rate, and system pressure, operators can identify potential issues before they escalate into major problems. This proactive approach to maintenance not only reduces repair costs but also ensures consistent product output and quality. Furthermore, the use of energy-efficient motors and variable frequency drives (VFDs) helps to minimize energy consumption, contributing to lower operational costs and a reduced environmental footprint.
In conclusion, baking soda material conveying lines are sophisticated systems that combine mechanical engineering, control technology, and material handling expertise to provide efficient and reliable transport solutions for industrial applications. The working principle, which may vary based on the specific design and application, is centered on the safe and controlled movement of sodium bicarbonate from storage to processing or packaging stages. Key features such as high efficiency, adaptability, and product purity make these systems essential for manufacturers in the baking soda industry. As a leading company in this field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored solutions that meet the evolving needs of the industry, ensuring that baking soda material conveying lines remain at the forefront of industrial material handling technology.