

Airborne Transport of Rare Earth Ore Powders: How to Efficiently Move Powdered Particulate Materials
Efficient and reliable material handling is a critical factor in the processing of rare earth ore powders. The traditional methods of manual or mechanical transport often face challenges such as dust generation, material degradation, and inefficiencies in handling fine particulate materials. Airborne transport, or pneumatic conveying, offers a modern solution to these challenges by utilizing air flow to move powders and granules through a system of pipes and equipment. This approach not only enhances safety and hygiene but also improves the overall productivity of rare earth processing facilities.

Introduction to Airborne Transport of Rare Earth Powders
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in providing advanced solutions for the airborne transport of rare earth ore powders. With a focus on innovation and technical excellence, HeadPowder has developed a range of systems tailored to the unique requirements of rare earth processing industries. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality engineering solutions.

The Role of Airflow in Efficient Material Handling
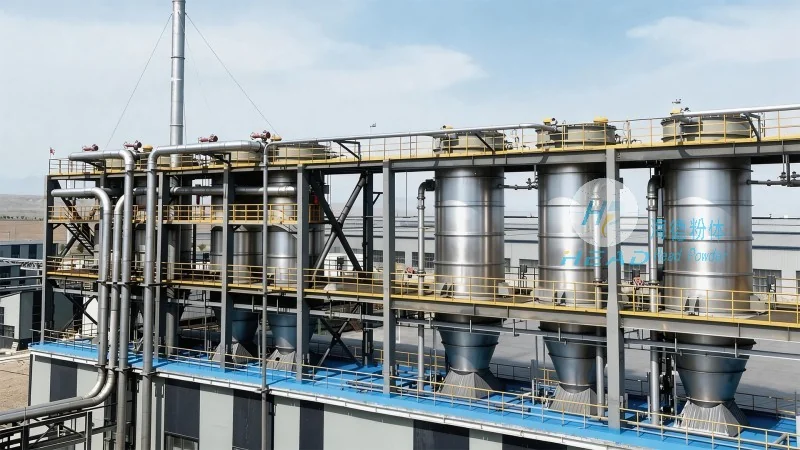
HeadPowder's airborne transport systems are designed to handle the specific properties of rare earth powders, which often include high value, sensitivity to moisture, and varying particle sizes. The company utilizes advanced pneumatic conveying technologies, including positive and negative pressure systems, to ensure optimal performance. These systems are equipped with features such as dust collection, material separation, and flow control, which help maintain the purity and integrity of the rare earth materials throughout the transport process.

Key Features of HeadPowder's Airborne Transport Solutions
The applications of HeadPowder's airborne transport solutions span various stages of rare earth processing, from ore crushing and grinding to material storage and packaging. In the crushing and grinding stage, the system efficiently conveys the fine powders from crushers and mills to storage silos or processing units. During the storage and packaging phase, the technology ensures that the powders are moved without degradation, preserving their quality for downstream processing or sale. The systems are also adaptable to different production scales, from small-scale pilot plants to large industrial facilities, making them suitable for a wide range of rare earth processing operations.
Technical Advantages for Rare Earth Processing
Operational benefits of using HeadPowder's airborne transport systems include reduced labor costs, minimized material loss, and improved workplace safety. By eliminating the need for manual handling of powders, the systems reduce the risk of dust exposure and related health hazards. Additionally, the automated nature of the process enhances consistency and reduces the potential for human error, leading to higher product quality and more efficient production cycles. The systems also contribute to better environmental management by containing dust and preventing contamination of the surrounding environment.
Conclusion and Company Overview
For industries dealing with rare earth ore powders, the choice of an efficient and reliable transport system is paramount. HeadPowder Engineering Co., Ltd. offers comprehensive solutions that leverage advanced pneumatic conveying technologies to meet the specific needs of rare earth processing. With a strong commitment to quality and innovation, HeadPowder provides systems that enhance productivity, safety, and material integrity. Based in Shandong, China, the company continues to be a leader in the development of airborne transport solutions for the rare earth industry, helping clients achieve their operational goals with greater efficiency and reliability.