

Sodium Hydroxide Powder Pneumatic Conveying: A Solution to Overcome Distance Limitations in Material Handling
For industrial applications requiring the efficient and reliable transport of sodium hydroxide powder over extended distances, traditional methods often fall short. The challenge of maintaining material integrity while ensuring consistent flow rates has long been a concern for process engineers. This is where advanced pneumatic conveying systems, specifically designed for sodium hydroxide powder, emerge as a transformative solution. By leveraging air to move bulk materials, these systems offer a versatile approach to material handling that surpasses the limitations of conventional methods.

HeadPowder, a leading provider in the field, specializes in the design, manufacturing, and implementation of pneumatic conveying solutions tailored to the unique demands of sodium hydroxide powder. With a focus on durability, efficiency, and safety, their systems are engineered to handle the corrosive and abrasive nature of this chemical while ensuring minimal product degradation. The company’s expertise lies in customizing systems that can accommodate varying distances, from short on-site transfers to long-distance transportation across industrial sites or even between facilities.
One of the key advantages of pneumatic conveying for sodium hydroxide powder is its ability to overcome distance restrictions. Unlike mechanical conveyors that may require multiple transfer points or suffer from material blockages over long runs, pneumatic systems use a continuous stream of air to maintain a consistent flow. This not only reduces the risk of clogging but also allows for smoother, more reliable transport, even over distances that would be impractical with traditional methods. The technology is particularly beneficial in environments where space is limited or where the material needs to be moved through complex layouts, such as in chemical plants, refineries, or manufacturing facilities.

HeadPowder’s solutions are built on robust engineering principles, incorporating high-quality components that can withstand the harsh conditions associated with sodium hydroxide. The systems are designed with corrosion-resistant materials to protect against the chemical’s effects, ensuring long-term operational reliability. Additionally, the company emphasizes safety features, including pressure relief valves and monitoring systems, to maintain compliance with industrial safety standards. These measures are crucial for industries where handling sodium hydroxide involves strict regulatory requirements and operational safety protocols.
Another significant benefit of pneumatic conveying is its flexibility in handling varying particle sizes and moisture content. Sodium hydroxide powder can present challenges due to its fine particle structure and potential for clumping, but modern pneumatic systems are equipped with features like air classifiers and agitators to maintain optimal flow. This adaptability makes the technology suitable for a wide range of applications, from bulk storage and transfer to precise dosing in production processes. The ability to integrate with existing industrial infrastructure further enhances the practicality of adopting pneumatic conveying for sodium hydroxide powder handling.
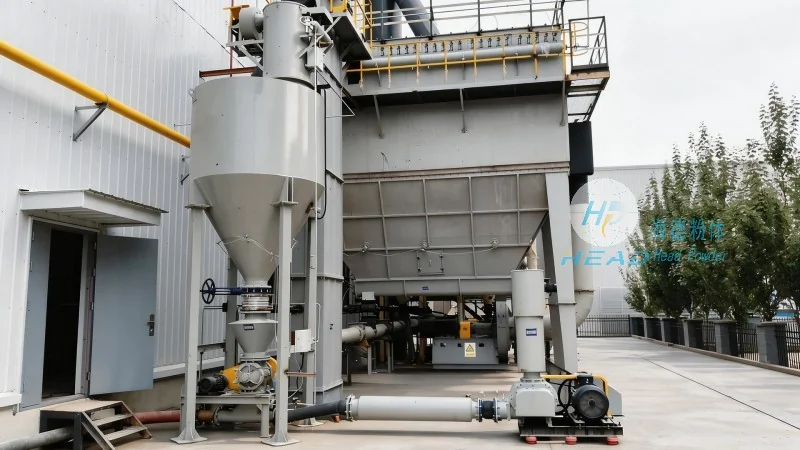
When considering the implementation of a pneumatic conveying system for sodium hydroxide powder, the importance of professional consultation and system design cannot be overstated. HeadPowder’s team of experts works closely with clients to assess their specific needs, including the required distance, material characteristics, and operational constraints. This collaborative approach ensures that the final system is optimized for performance, efficiency, and cost-effectiveness. By leveraging their experience in the industry, HeadPowder helps clients achieve significant improvements in material handling, reducing downtime, and enhancing overall productivity.

Moreover, the adoption of pneumatic conveying for sodium hydroxide powder contributes to operational efficiency and cost savings. By eliminating the need for multiple transfer points or extensive infrastructure, companies can streamline their material handling processes. The reduced risk of material loss or contamination also translates into lower operational costs and improved product quality. In addition, the energy efficiency of modern pneumatic systems, particularly when using optimized air flow and pressure control, further enhances the economic viability of the solution.
HeadPowder, based in Shandong, China, has established itself as a trusted partner in providing advanced material handling solutions. Their commitment to quality, innovation, and customer satisfaction has positioned them as a leader in the field. The company’s systems are not only effective in overcoming distance limitations but also in ensuring the safe and efficient transport of sodium hydroxide powder, meeting the demands of modern industrial applications. With a focus on continuous improvement and customer-centric service, HeadPowder continues to deliver solutions that help industries achieve their operational goals while maintaining the highest standards of safety and performance.