

Principle and Working Scene Characteristics of Intelligent Tonne Bag Feeding Station Pneumatic Conve
Intelligent tonne bag feeding stations equipped with pneumatic conveying lines represent a sophisticated solution for material handling in industrial settings. These systems are designed to efficiently transfer bulk materials from large bulk bags (tonne bags) into processing equipment or storage facilities. The integration of advanced automation and pneumatic technology ensures high accuracy, reliability, and minimal human intervention during the material transfer process.

Overview of Intelligent Tonne Bag Feeding Station Pneumatic Conveying Lines
At the core of these systems is the intelligent tonne bag feeding station, which is typically equipped with a pneumatic conveying line to transport bulk materials. The system combines features such as automatic bag opening, material discharge, and real-time monitoring to streamline the material handling workflow. This approach is particularly beneficial for industries dealing with powders, granules, or other bulk materials that require precise and controlled transfer.
Principle of Pneumatic Conveying in Tonne Bag Feeding Stations
The pneumatic conveying principle utilized in these systems involves the use of air to transport bulk materials through a pipeline network. The process typically operates under either positive or negative pressure, depending on the specific application requirements. In positive pressure systems, air is forced through the material, while in negative pressure systems, air is drawn away from the material. The intelligent feeding station incorporates advanced control mechanisms to regulate air pressure, flow rate, and material feed rate, ensuring consistent and efficient material transfer. The system may also include features like air filtration and dust collection to maintain a clean and safe working environment.
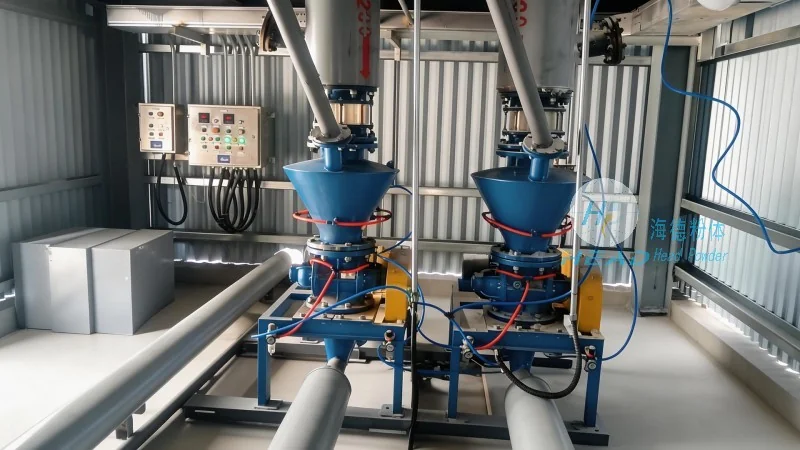
Working Scene Characteristics of Intelligent Tonne Bag Feeding Stations
The working scene characteristics of these systems are tailored to meet the diverse needs of industrial applications. For instance, in manufacturing facilities, the intelligent feeding station can be integrated with production lines to ensure a continuous supply of raw materials. In chemical processing plants, the system may be designed to handle hazardous materials with enhanced safety features, such as sealed bag handling and explosion-proof components. The flexibility of the pneumatic conveying line allows for horizontal, vertical, or inclined material transport, adapting to the layout of the facility. Additionally, the system can be equipped with sensors and automation controls to monitor bag status, material level, and operational parameters, providing real-time data for process optimization.

Advantages and Applications in Industrial Settings
The intelligent tonne bag feeding station with pneumatic conveying lines offers several advantages over traditional material handling methods. These include reduced labor costs due to automated operations, increased material handling efficiency, and improved safety by minimizing manual handling of bulk bags. The system is widely used in industries such as pharmaceuticals, food processing, chemicals, and minerals processing, where the handling of bulk materials requires precision and reliability. The integration of advanced technology ensures that the system can handle a wide range of materials, from fine powders to coarse granules, with consistent performance and minimal downtime.
Conclusion and Company Information
Intelligent tonne bag feeding stations with pneumatic conveying lines are essential equipment for modern industrial material handling. By combining advanced automation, pneumatic technology, and real-time monitoring, these systems provide efficient, reliable, and safe material transfer solutions. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing customized solutions tailored to the specific needs of industrial clients. With operations based in Shandong, China, the company leverages its expertise to deliver high-quality equipment that meets the demands of various industrial applications. The intelligent feeding stations and pneumatic conveying lines offered by HeadPowder are engineered to enhance productivity, reduce operational costs, and ensure compliance with industry standards.